
INDUSTRIAL AUTOMATION / PLC · HMI · MOTION
PLC, HMI programming
and industrial control
Siemens and Omron PLC and HMI programming, with variable frequency drive and servomotor integration. From a specific modification to the control system of a complete machine.
PROGRAMMING AND CONTROL
From the machine cycle
to everyday operation.
You can commission machine programming and control as a specific service, or include them in a complete mechanical, electrical and automation project.
- PLC sequence programming and modifications.
- HMI screens for operation, settings, jobs and diagnostics.
- Alarms, operating conditions and process interlocks.
- Integration of sensors, encoders, motors and drives.
- Data recording and export according to the application.
- Testing and commissioning within the agreed scope for each machine.
I develop electrical schematics and documentation in EPLAN as part of electrical and automation work, within the commissioned scope. I coordinate that documentation with the installed equipment, PLC program and HMI screens.


PLC AND HMI
Siemens and Omron.
Control for your machine.
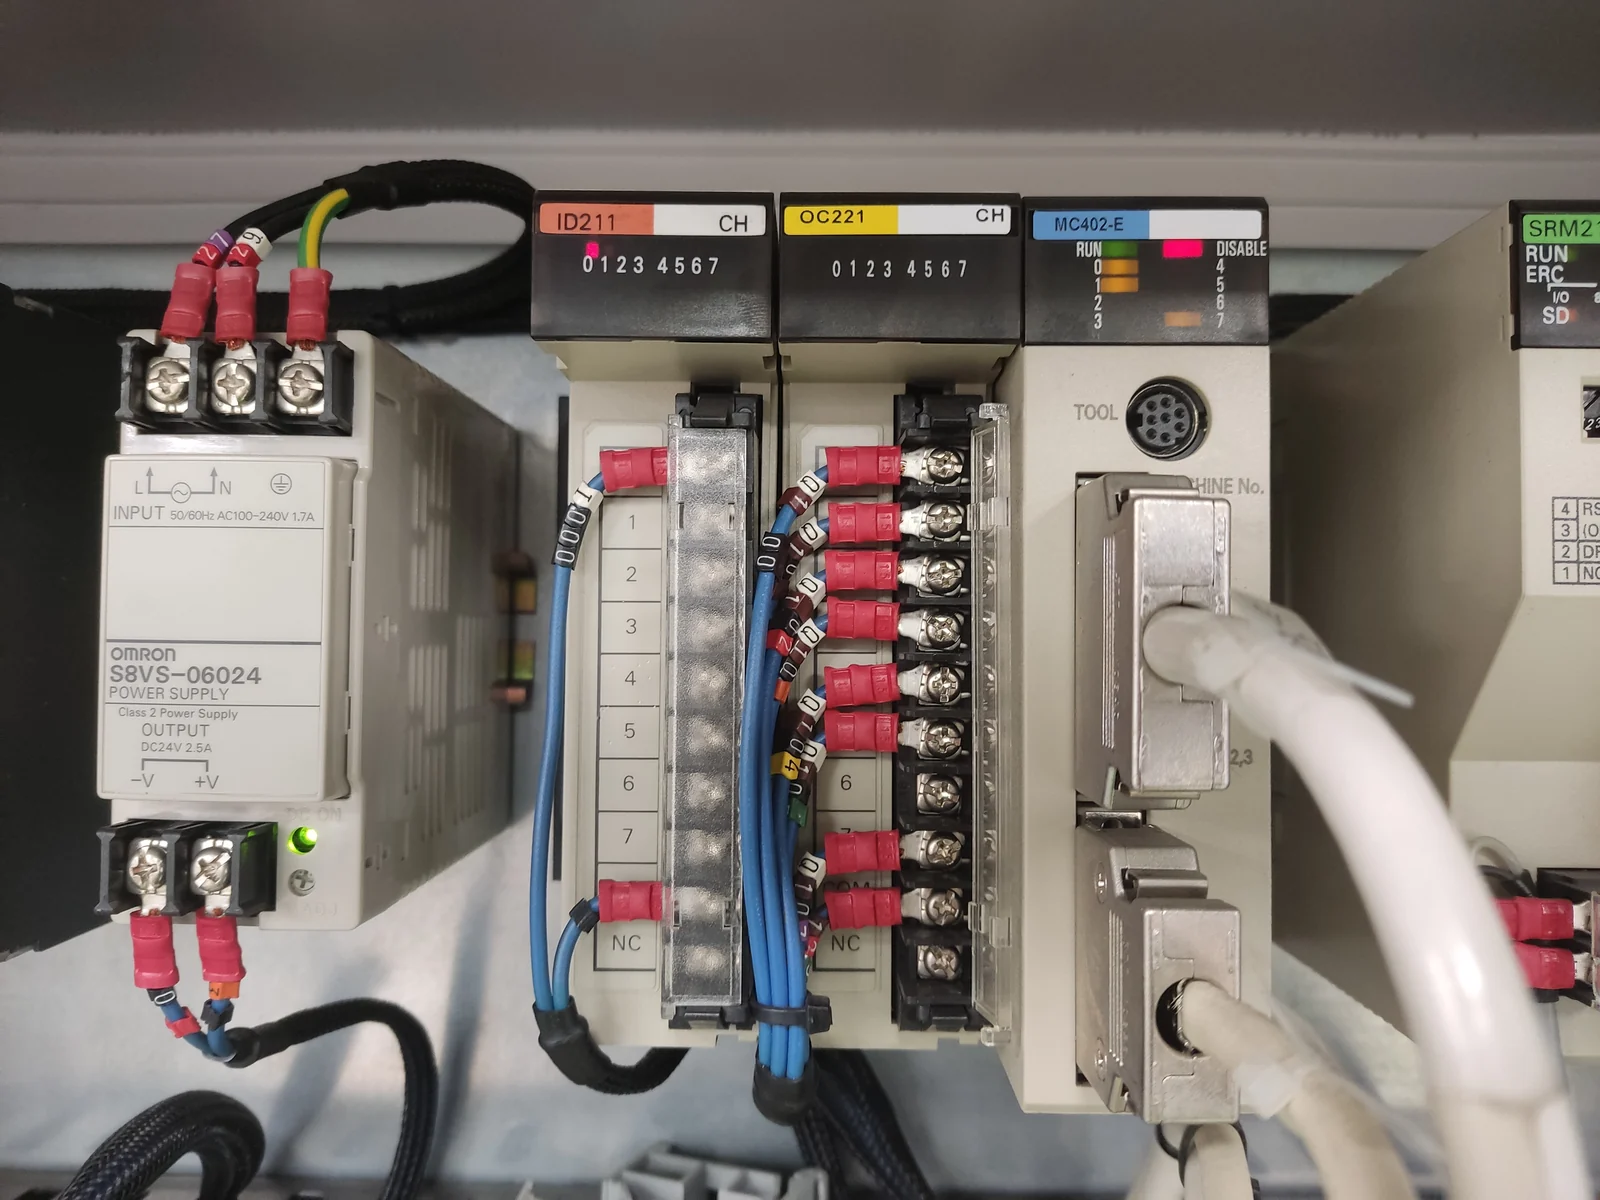
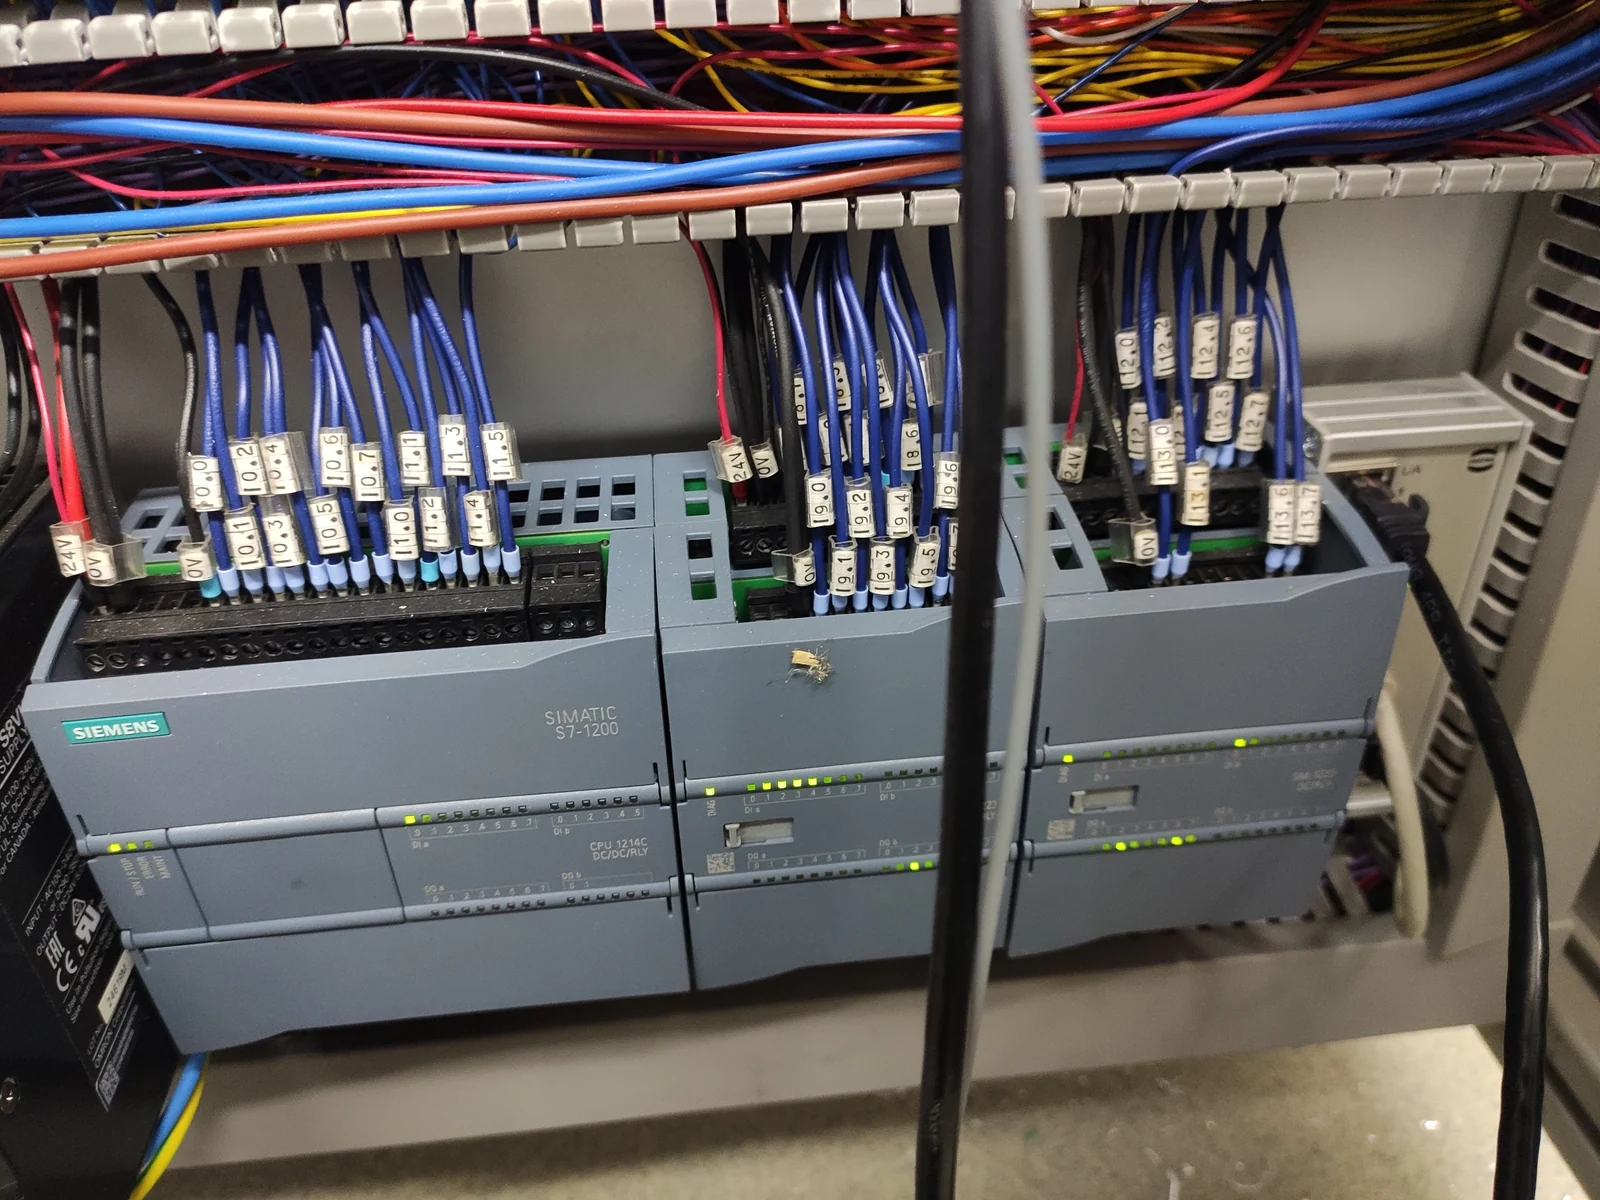
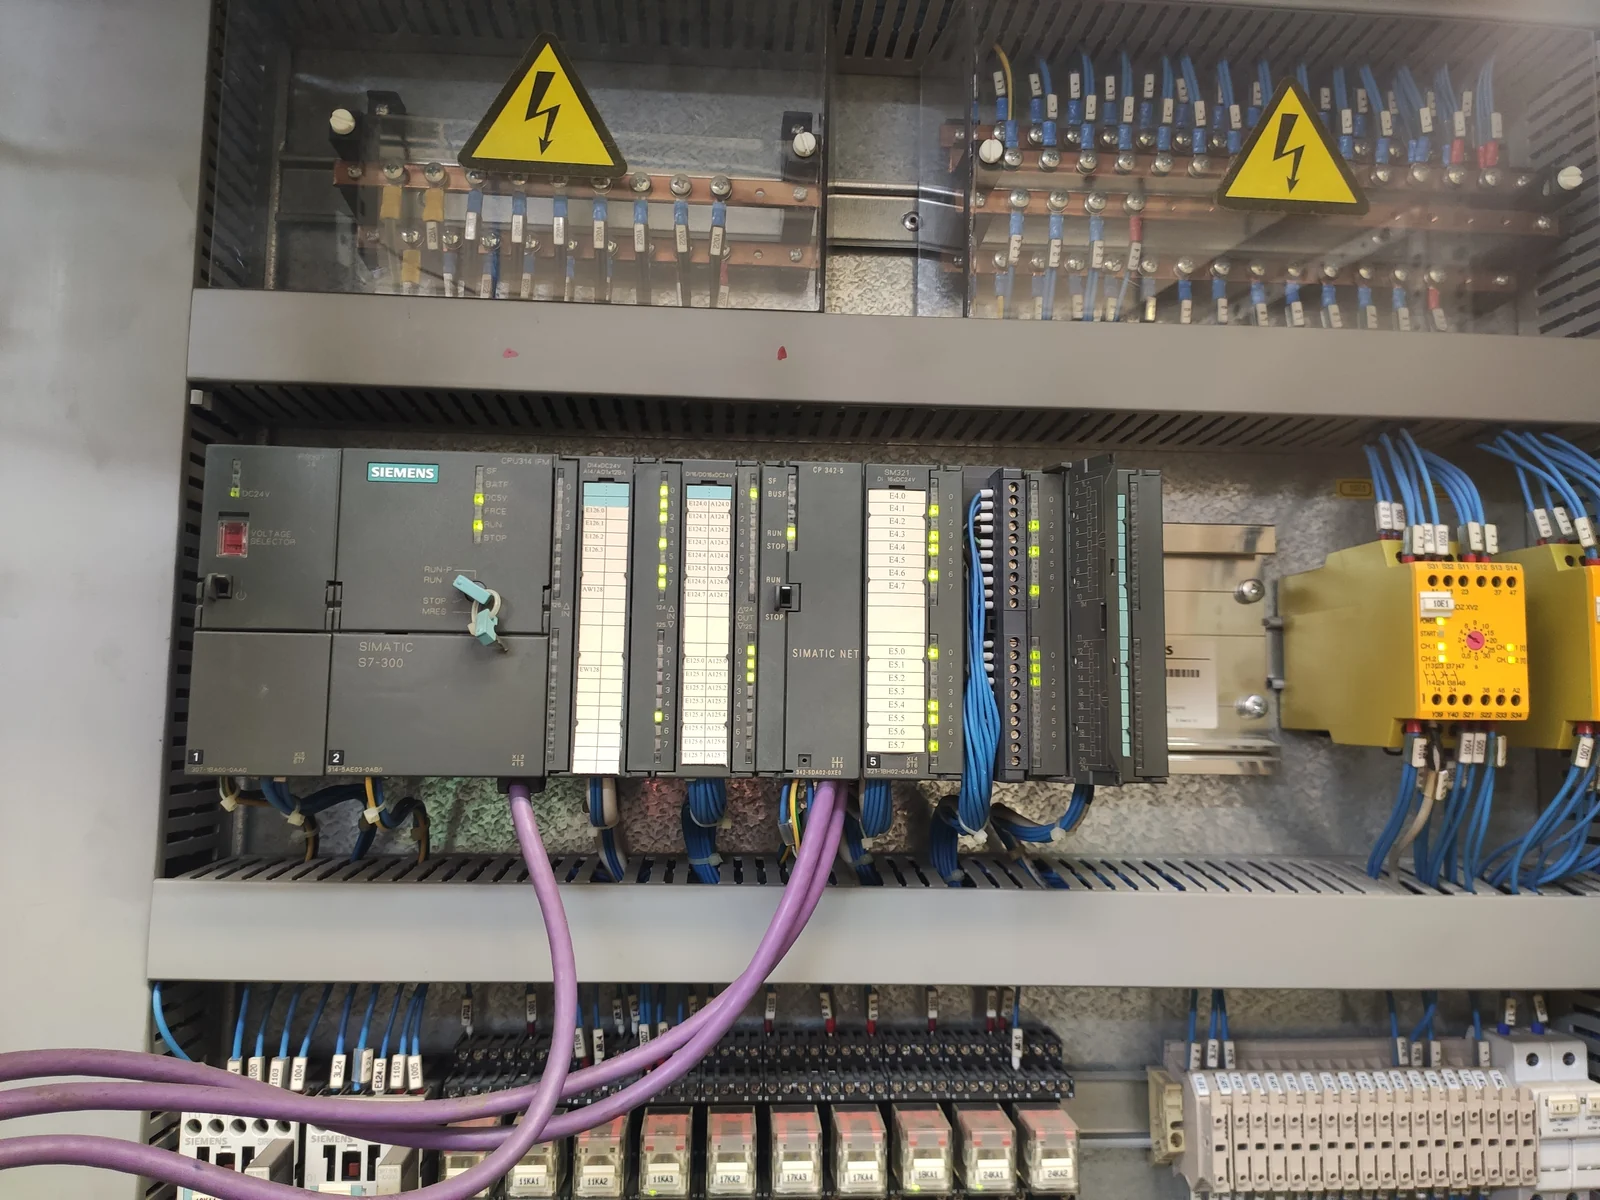
I work with Omron PLCs programmed using CX-Programmer and Siemens systems in TIA Portal, as well as older Siemens S7-200 systems.
The sequence and interface are developed together: what the machine must do, what the operator can adjust and what information helps them operate it and identify an issue.
Component selection and the scope of work depend on the installation, functions and available documentation.
MOTORS, DRIVES AND ENCODERS
The drive is also
part of the control system.
I work with variable frequency drives from Omron, Schneider Electric, Yaskawa and Lenze, alongside other equipment depending on the application.
I also work with Omron, Delta and other servomotor brands, depending on the equipment.
Three-phase motors, stepper motors and encoders are part of the drive and control solutions I integrate according to the needs of the machine.
Integration considers the motor, control method, speed references and process response. Parameter settings, adjustments and diagnostics are assessed as part of the complete system, together with the PLC and machine operation.
EXISTING MACHINERY
Change what is needed.
Keep what works.
A control modification can start with a machine already in service. Before intervening, I review its operation, installed equipment, available program backups and documentation.
I assess machinery retrofits and the migration of obsolete PLCs and HMIs: updating controls, replacing older equipment and integrating new functions while retaining useful components. Interfaces, program adaptations and commissioning tests are defined for each intervention.
Whether a program can be obtained from the device depends on its model, condition and available access.
DIRECT CONTACT
Understand your machine.
Define the work.
Start by telling me which machine you have, which PLC, HMI or drive it uses and what you need to resolve. Photographs of equipment references, diagrams and any program backups help define the intervention.
Site work in Barcelona and the Vallès area, with scope, travel and availability agreed for each job.
Real evidence
How it is applied.
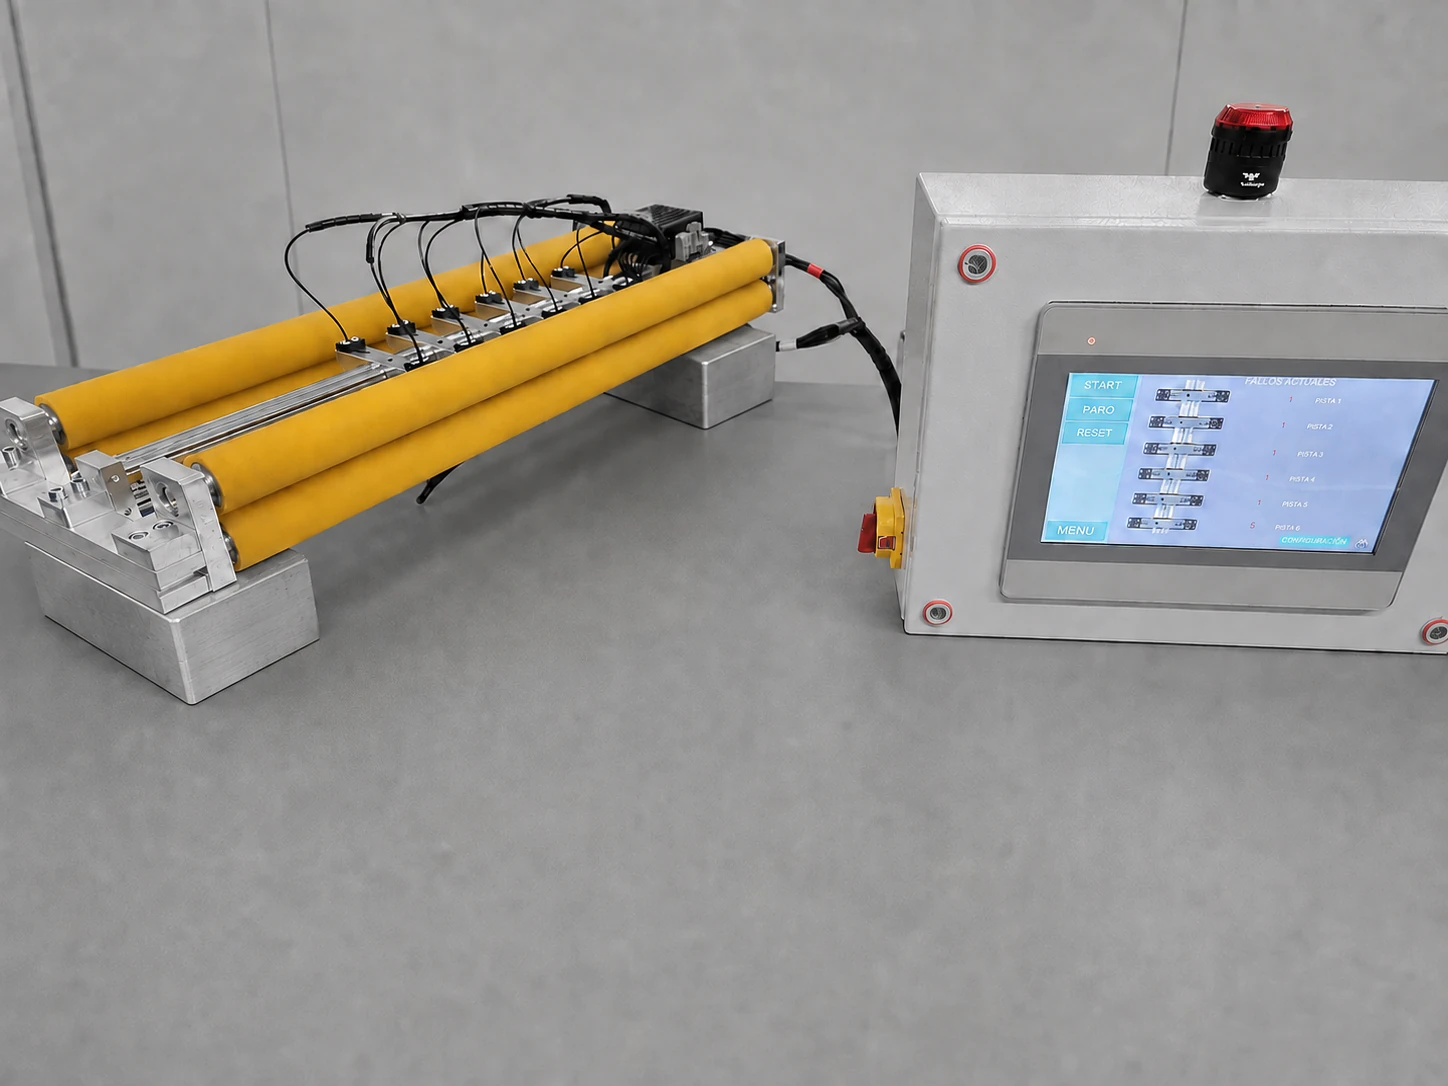
RV-510 logs incidents by lane; ALZA+ coordinates welding and RFID validation; CCPB7 integrates transport, encoding, printing and the response to inspection. In the latter case, the vision software comes from a specialist supplier.
Quality and inspection
Perforation inspection
Six-track perforation inspection, integrated into an existing printing line. Mechanics, sensors and controls working as one system.
Explore the case study ↗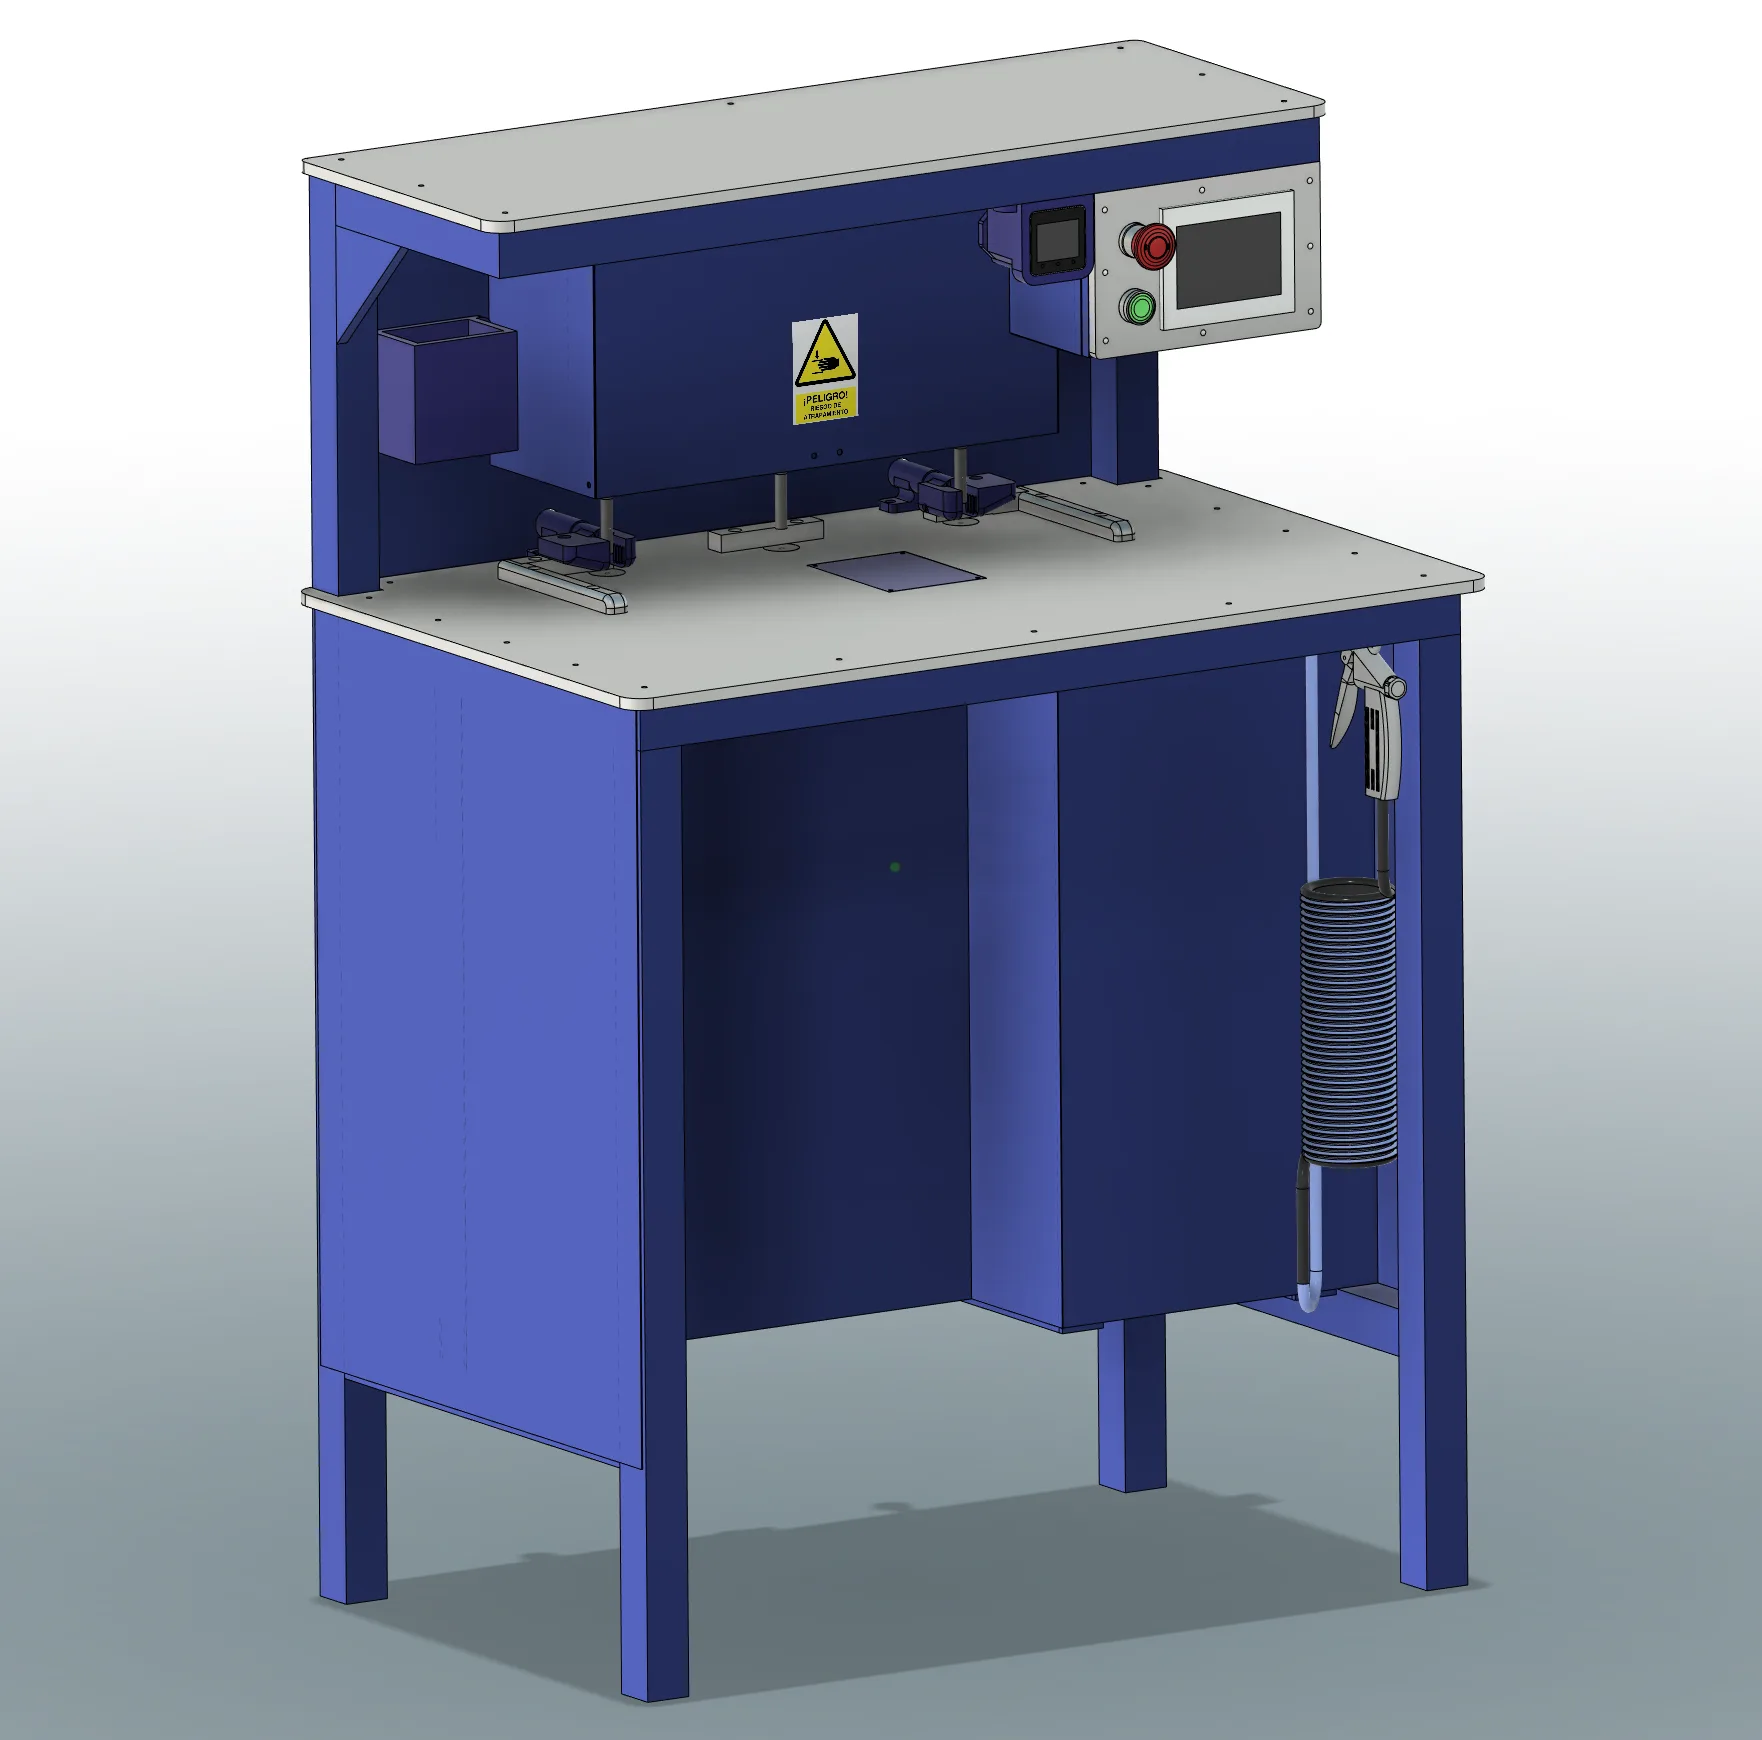
Automation and purpose-built equipment
Ultrasonic welding
Semi-automatic ultrasonic welding machine for multilayer stacks. From design and manufacturing to controls and improvements in service.
Explore the case study ↗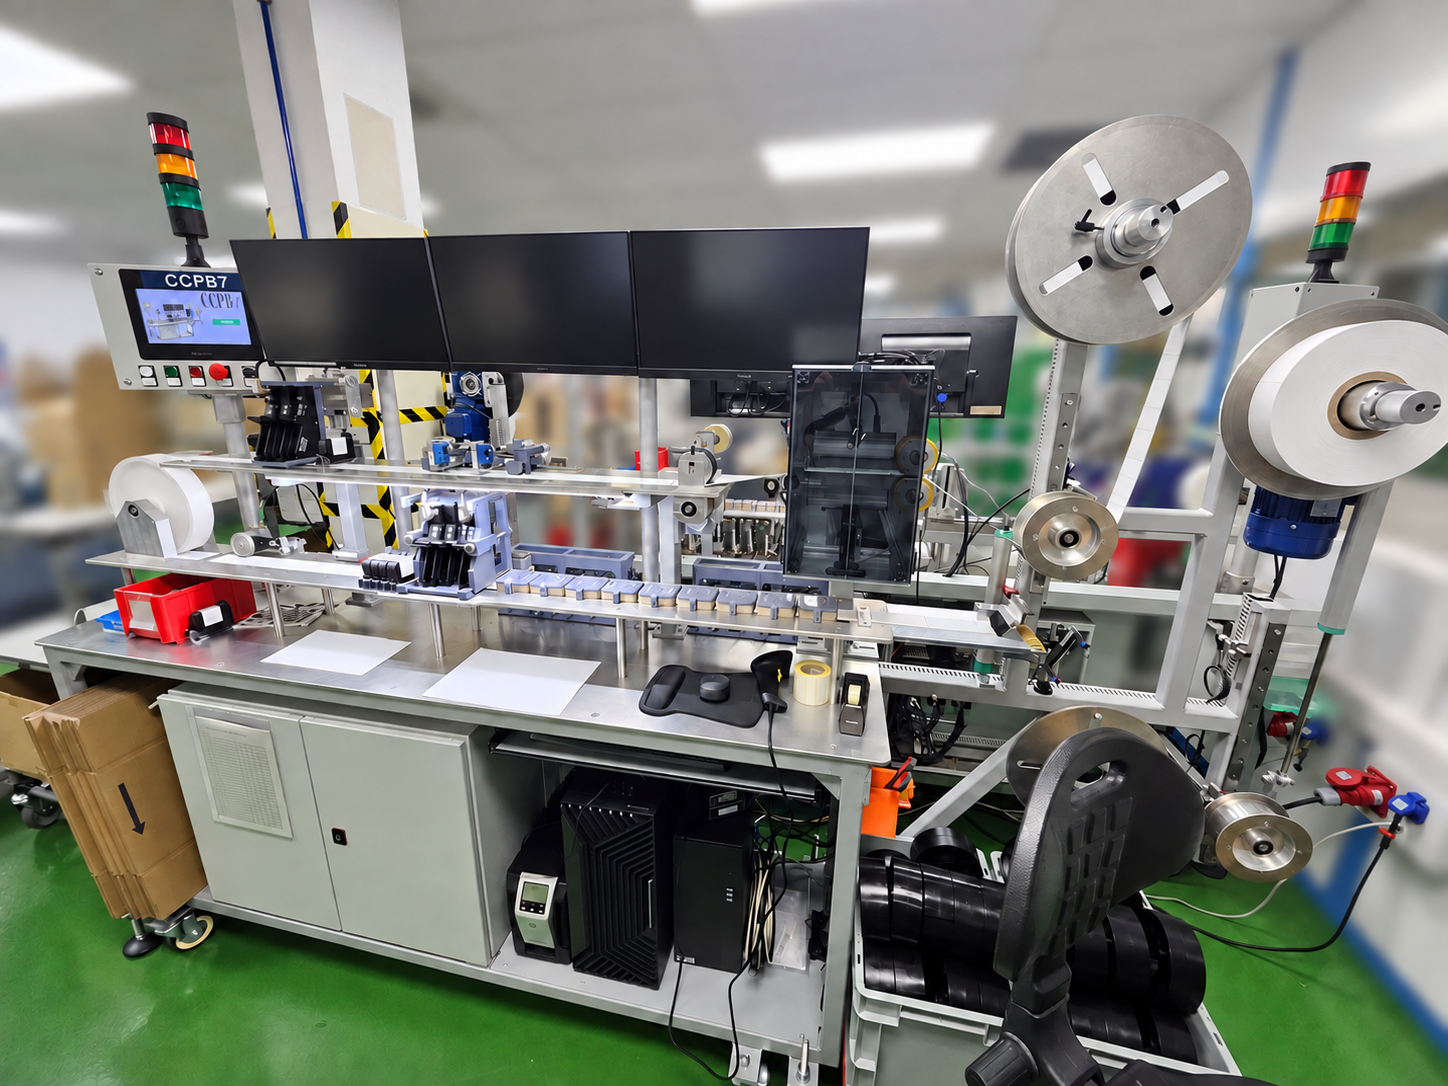
Automation and purpose-built equipment
RFID encoding, printing and inspection
RFID encoding, double-sided inkjet printing, vision inspection and rewinding. Six machines, with improvements extended across the series.
Explore the case study ↗Technology is the means.
Your need is the starting point.
View solutionsYour next step
What do you need to solve?
Tell me what you want to achieve and which part, equipment or process is involved. You do not need to have the solution worked out.